CNC Router for Acrylic
MNT (MEINAITE) CNC routers mill acrylic, polycarbonate and PVC sheet with O-flute carbide tooling — chip cutting, not heat, so the sheet never melts, crazes or gasses off.
- No melt, no chatter — single-flute O-geometry clears chips at 24,000 RPM instead of rubbing
- Thick sheet a laser can’t take — 20–50 mm acrylic with no taper and no scorched face
- Cuts what a laser must not — polycarbonate and PVC mill clean; a CO2 beam burns one and gasses the other
Milling Acrylic Without Melting It
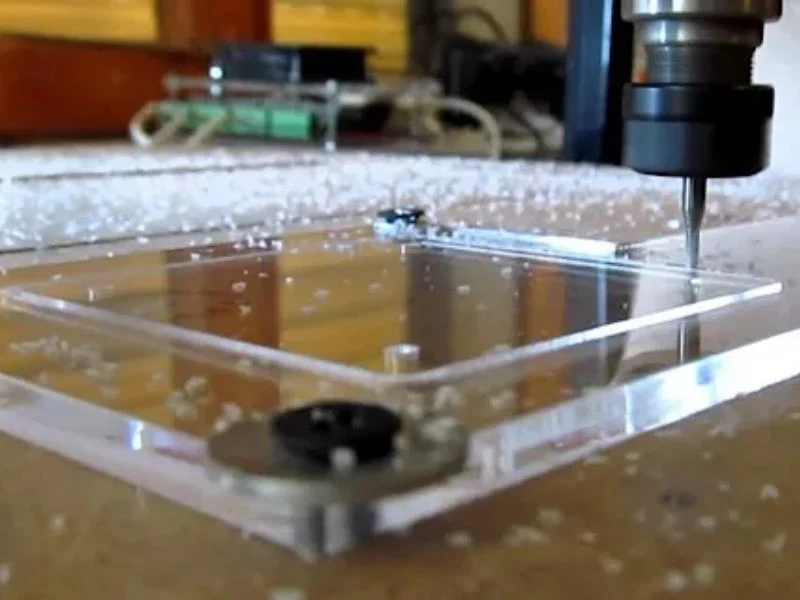
Acrylic punishes the wrong tooling. Run a standard two-flute wood bit and the chips re-weld to the cut face; run too slow and the bit rubs instead of shears, and the sheet melts onto the cutter. The fix is not a bigger machine — it is a single-flute solid carbide O-flute bit, a feed rate high enough to keep the chip load up, and a rigid gantry that will not chatter at 24,000 RPM. That is what an MNT CNC router is set up to do.
Where a router beats a laser, and where it doesn’t. For thick sheet, pockets, grooves, 3D relief, polycarbonate and PVC, a router wins outright. For thin sheet where you want a glass-clear edge with zero post-processing, a CO2 laser wins. MNT builds CNC routers and fiber lasers for metal — not CO2 lasers for plastics — so if thin, polished-edge acrylic is your whole job we will say so. Most acrylic fabricators need both capabilities and buy the router first, because it is the one that also machines ACP, wood and aluminium. See the full MNT CNC router range or the heavier machining centres. If the wood-panel half is the bigger half of your work, that is a different buying decision — sheet yield and nesting rather than edge finish decide it — and it has its own page: cabinet making CNC machine.
Machining thick 6061 plate or structural aluminium rather than acrylic and thin sheet? That is a rigidity job for a machining centre — see the CNC router for aluminum page, which walks the router-to-machining-centre gradient for metal.
Cutting G10, FR-4 or Garolite rather than acrylic? Same T-series spindle, opposite failure mode: acrylic melts if you feed too slowly, glass-filled laminate destroys the cutter if you feed too slowly. See CNC router for G10 and FR-4.
Running a sign shop rather than a plastics shop? This page is the material view — how acrylic behaves under a cutter, and the feeds and tooling that keep the edge clean. The trade view — substrate mix, print-to-cut registration and what a shop actually quotes — is on our CNC router for sign making page.
Machine specifications compared. Acrylic rewards spindle speed over spindle power — a flame-polished edge comes from a high RPM and a single sharp O-flute, not from pushing harder. The T5 gives you a rigid, stress-relieved bed for heavy routing; the T7 gives you higher spindle speed and nine tool stations for jobs that mix acrylic with board and knife work.
| Specification | T5 | T7 |
|---|---|---|
| Working area | 1300 × 2500 mm | 1300 × 2500 mm (T7-1325) · 2000 × 3000 mm (T7-3020ATC) |
| Spindle | 5.5 kW water-cooled | Water-cooled, 40,000 RPM |
| Tool changer | — | Linear · 9 stations (T7-1325), 6 (T7-3020ATC) |
| Drive system | Imported precision racks (X/Y), ground ball screw (Z) | Leadshine servo (X/Y/Z) |
| Positioning accuracy | — | 0.05 mm / 300 mm |
| Bed | Inline welded, quenched & stress-relieved | — |
| Worktable | Vacuum hold-down | 4-zone vacuum, 500 kg load |
Acrylic and Plastics We Machine
Cast Acrylic (PMMA)
- Formats: Cast PMMA sheet, 2–30 mm, clear, coloured and opal
- Watch out: Cast is the forgiving one — the trap is assuming extruded behaves the same way and running the same program on both
- How we cut it: Higher molecular weight and no internal stress means it chips away rather than smearing; the finish comes off the bit almost polish-ready
Extruded Acrylic (XT)
- Formats: Extruded PMMA sheet, 2–20 mm
- Watch out: Softer and far more prone to melting — run cast parameters on XT and the chips weld themselves back into the cut
- How we cut it: Lower step-down and higher feed rate keeps chip load up: same clean edge, different recipe
Polycarbonate (Lexan)
- Formats: PC sheet, 2–20 mm, clear and impact grades
- Watch out: A CO2 laser turns PC brown and brittle at the cut line — and brittle is the one thing a machine guard must not be
- How we cut it: Milled with a sharp O-flute it cuts clear and keeps full impact strength, which is why guards get routed, not lasered
PETG, PVC & ABS
PVC must never meet a laser — it releases chlorine gas that corrodes optics and frame. Routing is the safe route for expanded PVC, PETG and ABS on the same bed and the same setup.
Feeds, speeds and tooling here are MNT's own T-series settings: 18,000-24,000 RPM, 2-7.6 m/min, single-flute O-flute carbide.
Signage, Displays and Guards Routed From Acrylic
Light Boxes & Channel Letters
Face panels, returns and diffusers cut to contour on a 1300 × 2500 mm bed, so a full sheet is machined in one placement with consistent letter spacing.
Retail Display & POP Fixtures
Slots, tabs and pockets machined in the same pass as the outline — parts snap together without secondary drilling or routing jigs.
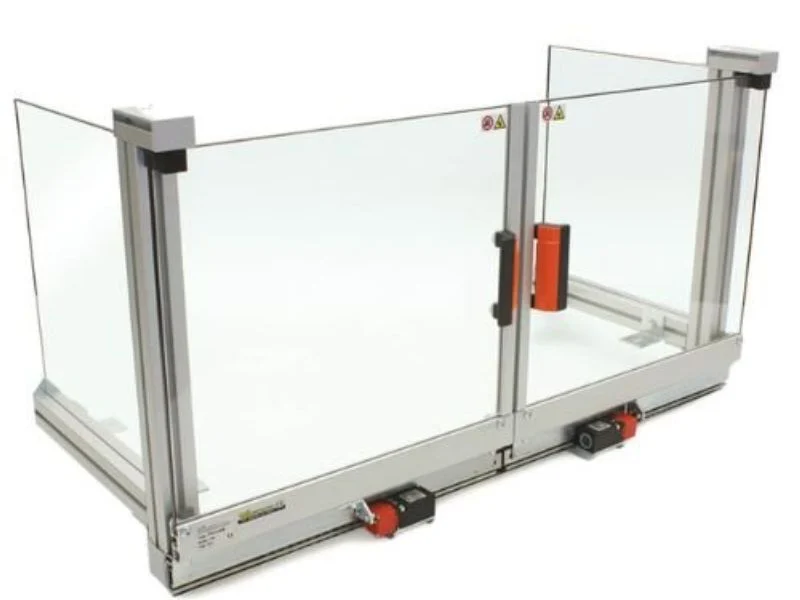
Machine Guards & Safety Shields
Polycarbonate guards keep full impact strength because there is no heat-affected zone — a lasered PC edge goes brittle exactly where the guard needs to hold.
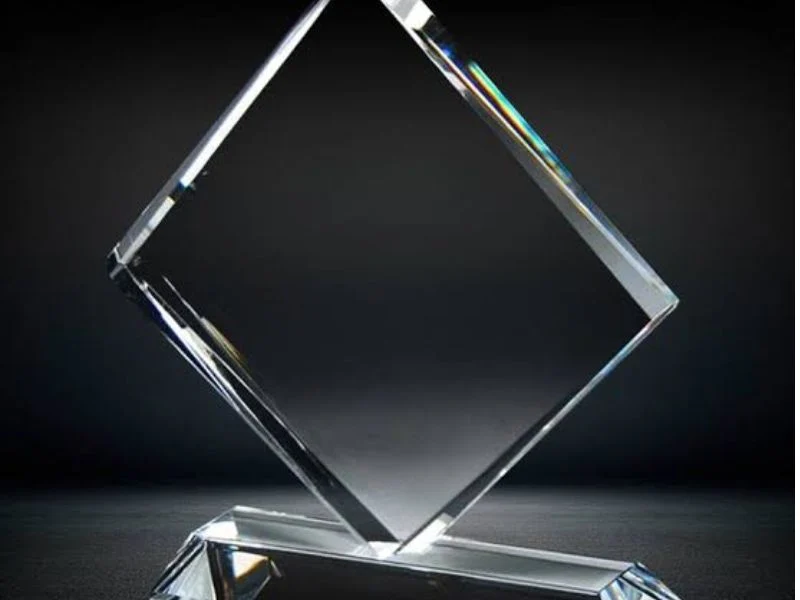
Awards, Plaques & Deep Engraving
V-carve and 3D relief down to 10 mm deep — depth a laser cannot reach, on cast acrylic that polishes to optical clarity.
Bed size, registration accuracy and cut depth measured on a T5 with a 1300 x 2500 mm table and CCD camera registration.
Recommended MNT Machines
Acrylic is milled, not knife-cut — these are the T-series routers set up for plastics, with O-flute tooling and the rigidity that stops chatter.
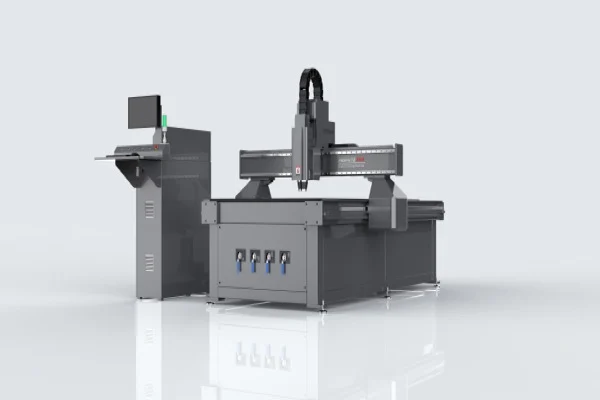
T5 Precision CNC Router
- Cuts: Cast and extruded acrylic, polycarbonate, PVC, PETG, ABS
- Specs: Precision gantry · single-flute O-flute tooling · 18,000–24,000 RPM · ≤ 20 mm plastics
- Best for: Shops where edge quality on plastics matters more than raw bed size
- Price: From $8,900
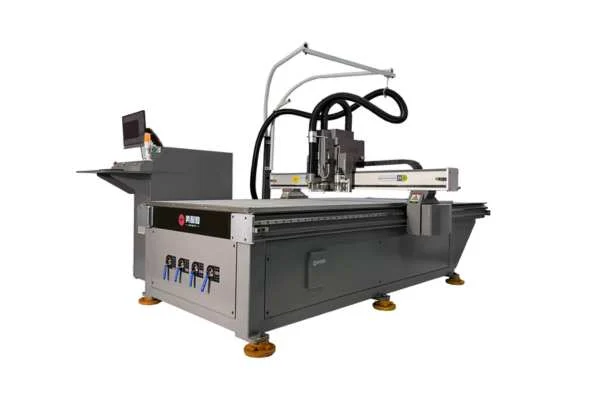
T7 ATC Digital Engraving & Cutting Machine
- Cuts: Acrylic, ACM, MDF, wood, composite panel
- Specs: Automatic tool change · cut-out, V-carve and drill in one job · vacuum table
- Best for: Jobs needing several tools per part without an operator at the spindle
- Price: From $17,800
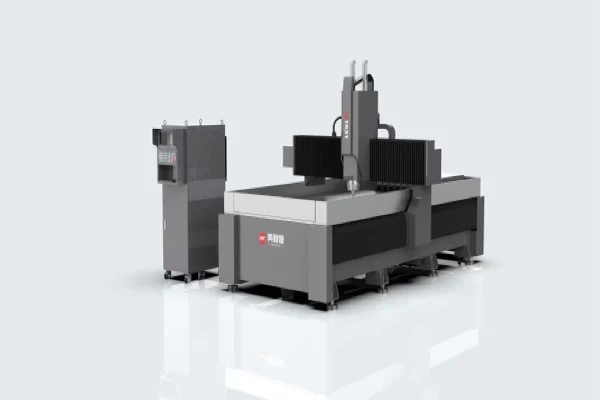
M-Series CNC Machining Centre
- Cuts: Thick acrylic, aluminium, copper, composite plate
- Specs: Heavy welded frame · higher spindle torque · 30–50 mm plastics routine
- Best for: Plate work where a router gantry starts to flex
T-series routers run the same control platform; models differ by gantry rigidity, bed size and tool changer.
Pick by Thickness, Material and Edge
“Using a router for acrylic sucks — it melts or chatters.” That complaint is real, and it is almost always tooling and feeds, not the machine: a two-flute wood bit at a timid feed rate will melt any acrylic. With a single-flute O-flute at the right chip load, on a gantry rigid enough not to chatter, a router cuts acrylic cleanly all day. Here is the honest split against the alternatives.
| Factor | CNC router (MNT) | CO2 laser | Table saw / hand |
|---|---|---|---|
| Thick acrylic (20–50 mm) | Yes, multi-pass | Taper & scorching past ~20 mm | Straight cuts only |
| Edge straight off the machine | Matte / frosted | Glossy, flame-clear | Rough, needs finishing |
| Polycarbonate (Lexan) | Cuts clean | Burns brown, unusable | Chips |
| PVC / expanded PVC | Cuts clean | Releases chlorine gas — corrodes optics | OK |
| Heat-affected zone | None (chip cutting) | Yes — internal stress, crazing risk | None |
| Pockets, grooves, V-carve | Yes, 3D toolpaths | Surface engraving only | No |
| Kerf | 3–6 mm (bit diameter) | ~0.2 mm | 3 mm |
The short version: thin sheet, glass edge, no post-processing → CO2 laser. Thick sheet, pockets, 3D depth, polycarbonate or PVC → CNC router. Searching for an acrylic cutting machine and unsure which side you are on? Send us the part and we will tell you which tool it belongs to, even when the answer is not ours.
Why Acrylic Fabricators Choose MNT
Distributor or OEM partner? Territory, spare-parts commitment and technical training are what decide whether a machine is worth carrying. Talk to us about partnership.
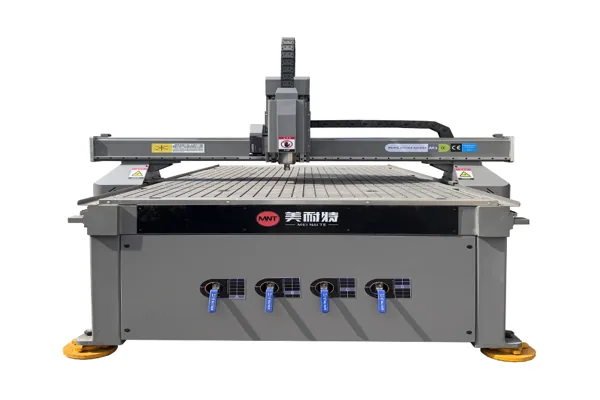
Set Up for Plastics, Not Just Wood
- O-flute plastic tooling, chip-load presets and mist cooling supplied with the machine
- Rigid welded gantry — the chatter that ruins acrylic edges starts with a flexing frame
- For distributors: almost every sign shop already outsources acrylic work, so the payback maths writes itself — you are quoting against an invoice they already pay every month
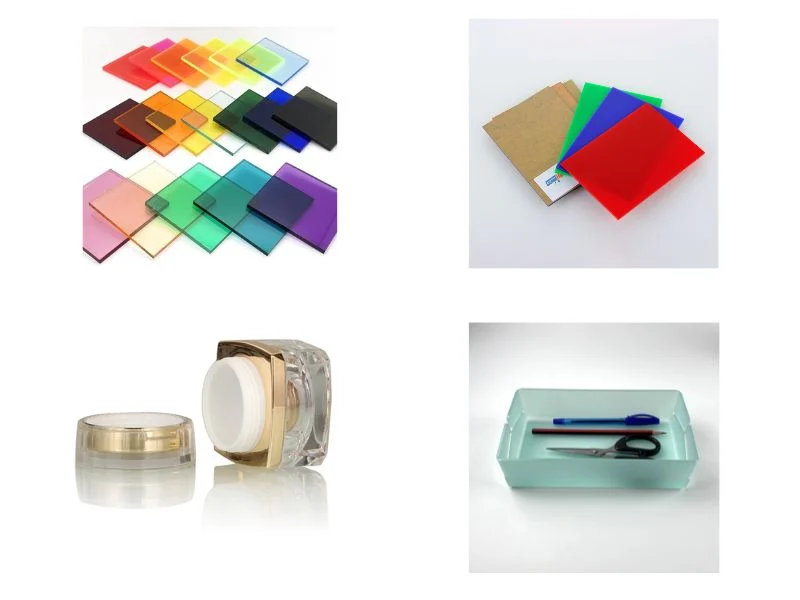
One Bed, Every Sign Substrate
- Acrylic, polycarbonate, PVC, ACP, wood and aluminium on the same table
- ATC models change from cut-out bit to V-carve to drill without an operator at the spindle
- For distributors: spare-parts commitment, territory and technical training are the three things that decide whether a machine is worth carrying — all three are set out on our partnership page
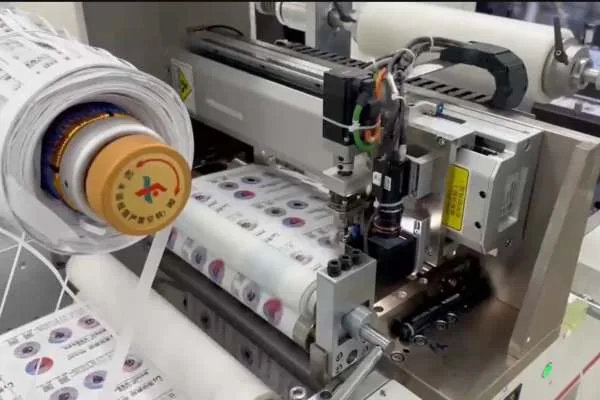
Vision Contour Cutting
- CCD camera follows printed registration marks for cut-to-print acrylic panels
- Compensates print stretch and skew so long runs stay square
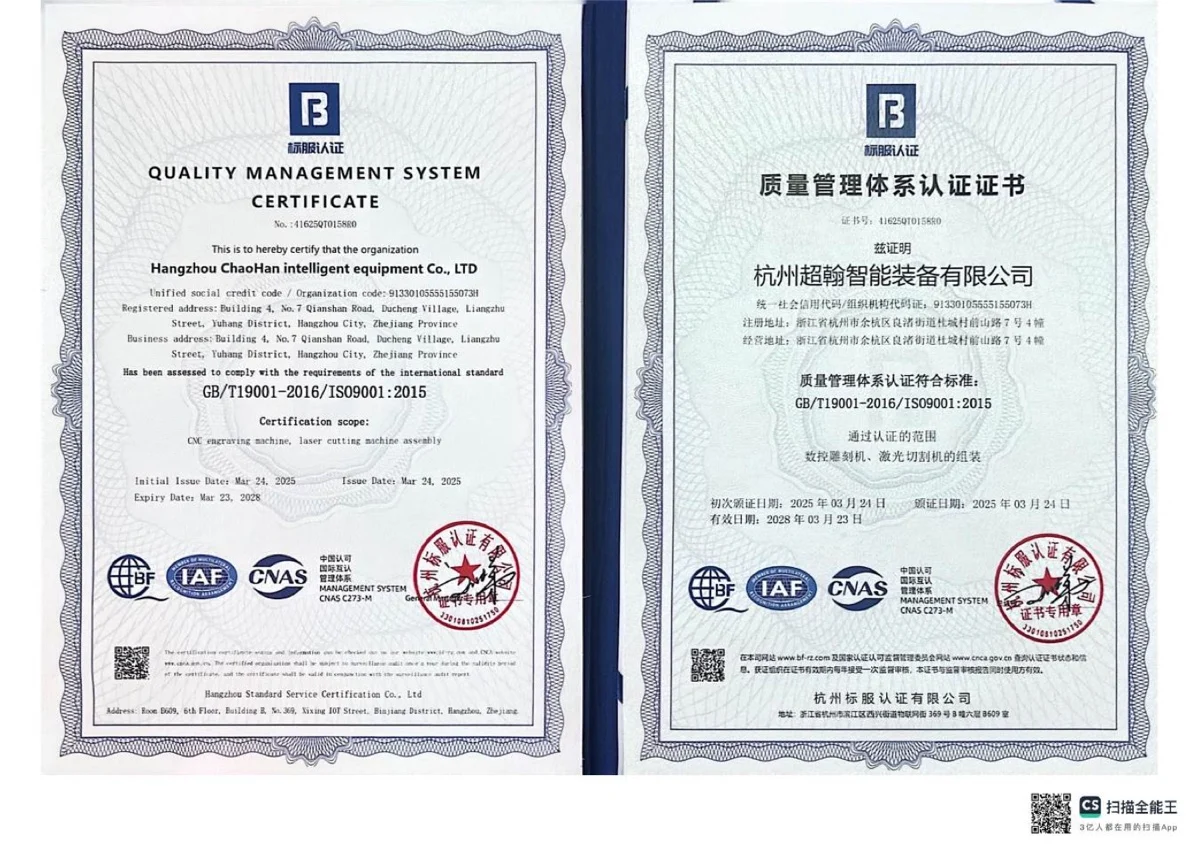
CE + ISO — Send Your Acrylic for a Free Test Cut
- CE-marked and ISO 9001 certified — built by Hangzhou Chaohan, not traded
- Send your sheet and file; we machine a free sample and return the edge photos
- 12-month warranty, lifetime remote support, tooling shipped worldwide
CE-marked and ISO 9001:2015 certified. Built by Hangzhou Chaohan Intelligent Equipment, not traded. Certificates on request.
Frequently Asked Questions
Can a CNC router cut acrylic without melting it?
Yes — melting is a tooling and feed problem, not a material limit. Use a single-flute solid carbide O-flute bit, keep the spindle around 18,000–24,000 RPM and push the feed to 2–7.6 m/min (75–300 ipm) so the bit shears chips instead of rubbing. Step down about half the bit diameter per pass. Get those three right and the chips fly clear and the edge stays crisp; get them wrong and any router will weld the chips back onto the cut face.
CNC router or laser cutter for acrylic?
Choose by thickness and edge. A CO2 laser gives a glass-clear polished edge with no post-processing and is the better tool for thin sheet up to about 20 mm. A CNC router handles thick sheet up to 50 mm without taper, machines pockets, grooves and 3D relief, and is the only option for polycarbonate and PVC. MNT builds CNC routers and fiber lasers. Note that fiber and CO2 are not interchangeable: a fiber laser’s 1064 nm beam passes straight through acrylic instead of being absorbed, so it cuts metal but not plastics — only a CO2 beam at 10,600 nm cuts acrylic. We do not build CO2 lasers, so if your work is all thin, polished-edge acrylic, a CO2 supplier will serve you better.
Cast or extruded acrylic — which machines better?
Cast acrylic (PMMA) machines noticeably cleaner. It has higher molecular weight and no extrusion stress, so it produces true chips and resists melting. Extruded (XT) sheet is cheaper and more widely stocked but softer — it needs a lighter step-down and a higher feed rate to stay clean. Both cut well on the same machine with the right recipe.
What bit should I use to cut acrylic?
A single-flute solid carbide O-flute (sometimes called a plastic-cutting spiral). The polished, highly rounded flute clears the chip completely instead of packing it into the kerf, which is what stops heat building at the cut line. Two-flute wood bits, downcut spirals and ball noses all trap chips in acrylic and cause melting.
How do I get a polished edge after routing?
A router leaves a matte or lightly frosted edge. For optical clarity, flame-polish with a propane or hydrogen torch in a single steady pass, or wet-sand up through 800–2000 grit and buff. Cast acrylic polishes far better than extruded. If every part must be glass-clear straight off the machine with no second operation, that is the case for a CO2 laser rather than a router.
How thick acrylic can a CNC router cut?
1–50 mm in multiple passes on our standard T-series, and thicker on the machining-centre models. Unlike a laser, thickness costs you cycle time but not edge quality — there is no taper and no scorching at 30 or 50 mm, which is exactly where a CO2 beam starts to fail.
How much does a CNC router for acrylic cost?
Production machines run roughly USD 6,000 for a 1300 × 2500 mm 3-axis router to USD 30,000+ for an ATC model with vision registration and vacuum zoning; heavy machining centres go higher. Desktop routers at USD 200–1,500 will cut acrylic but lack the rigidity and bed size for daily fabrication work. Tell us your sheet size and monthly volume and we quote factory-direct.
Can the same machine cut ACP, wood and aluminium?
Yes — that is the main reason sign shops buy a router before a laser. The same spindle machines acrylic, polycarbonate, PVC, aluminium composite panel, wood and aluminium sheet; only the bit and the feed recipe change.
Machining Plastics — Technical Guides
Acrylic is one of several plastics that reward the right tooling and punish the wrong one. These guides cover material choice and when a router beats the alternatives.
Machinable Plastics: PTFE vs POM vs PEEK vs Nylon
How the common machinable plastics differ in tooling, feeds and finish — useful before you switch material.
CNC Router vs Waterjet for Thick PTFE Plate
Router versus waterjet on thick plastic plate — the same trade-offs that decide router versus laser on acrylic.
Start Your Acrylic Machining Project
Send your sheet type (cast or extruded), thickness, part drawing and monthly volume — we recommend the right router and tooling and reply within 24 hours.