Carbon Fiber Cutting Machine
MNT (MEINAITE) C-series digital knife cutters ply-cut dry carbon fabric, prepreg, aramid and glass reinforcement — vacuum-held, nested, labelled, ready for layup.
- Oscillating and drag knife — clean sheared edges with no fraying and no heat-affected zone
- Nesting that protects margin — prepreg is the most expensive material on your floor
- Zone vacuum + conveyor — holds slippery, tacky and biased fabric flat through the cut
Two Different Jobs Get Called "Carbon Fiber Cutting"
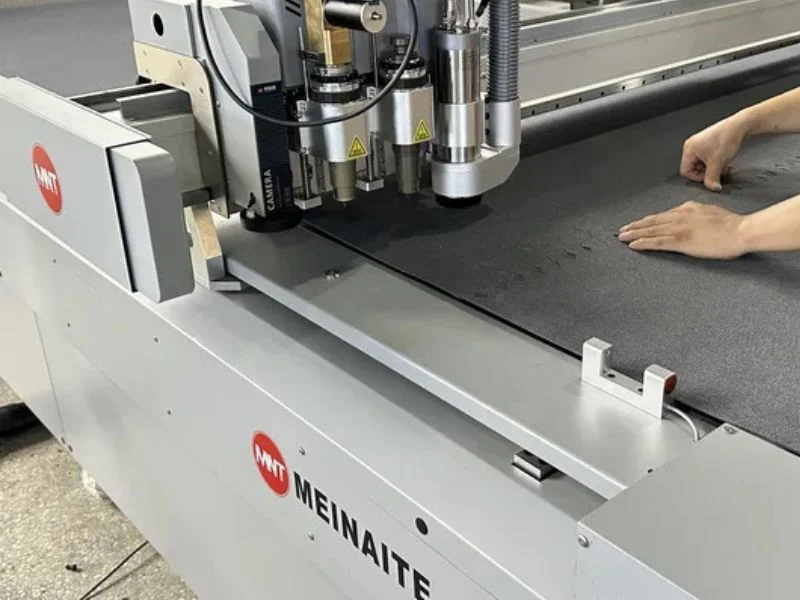
Search for a carbon fiber cutting machine and you get two unrelated answers, because two unrelated jobs share the name. Cutting the reinforcement before layup — dry fabric, prepreg, aramid, glass — is a knife job. Machining a cured laminate after autoclave is a diamond-tooling or waterjet job. A machine that is excellent at one is useless at the other — laminate suppliers such as DragonPlate sell the cured sheet that belongs on the second side of that line.
This page is the first job. The C-series is a digital knife cutter: a vacuum table, a conveyor, and a head carrying an oscillating or drag blade that shears the fabric against the belt. If you need to trim and drill a cured part, that is a spindle job rather than a knife job — and we build that machine too: see our CNC router for G10, FR-4 and epoxy glass laminate.
Why plies get cut on a knife table
- Zero kerf. A blade removes no material. On prepreg at hundreds of dollars per square metre, the kerf a laser or router burns away is money the nest never gets back.
- No heat. Laser cutting carbon fabric burns the resin, scorches the fibre and releases fumes; the charred edge compromises the bond line. A knife leaves the resin chemistry untouched.
- Nesting and labelling. Plies come off the table numbered and in kit order, which is what actually shortens layup — not raw cutting speed.
- Repeatability. Hand-cut plies vary; a ply booked at ±0.1 mm drops into the tool the same way every time, and that shows up in part weight consistency.
Bias-cut fabric distorts if it moves at all, and prepreg is tacky and usually cold out of the freezer. Both are hold-down problems before they are cutting problems — which is why the vacuum zoning matters more on this material than the blade does.
Cutting glass reinforcement rather than carbon? The fiberglass cutting machine runs the same knife platform, but glass fibre is cheap and cut in volume — there the economics are blade life and throughput, not the nesting yield that dominates costly carbon prepreg.
Machine specifications compared. Dry carbon fabric and prepreg are abrasive rather than thick, so the question is blade life and fibre pull, not depth. The rotary wheel tool shears continuous fibre without fraying the ply edge and is an option on all three; table size then decides whether a full-width ply fits in one nest.
| Specification | C6090 | C2516T | C3232 |
|---|---|---|---|
| Cutting area | 600 × 900 / 600 × 1200 / 900 × 1200 mm | 2500 × 1600 mm | 3200 × 3200 mm |
| Carbon fabric & technical textile | ≤ 10 mm | ≤ 10 mm | ≤ 10 mm |
| Rotary wheel tool | Optional | Optional | Optional |
| Pneumatic oscillating tool (POT) | Optional | Optional | Standard |
| Cutting speed | 300–1800 mm/s | 300–1800 mm/s | 300–1800 mm/s |
| Hold-down | Aluminium honeycomb, vacuum | Vacuum adsorption | Vacuum adsorption |
| Continuous belt feeding | Yes | Yes | Yes |
| Typical composite job | Test plies, small kits | Ply kitting, mixed materials | Full-width broadgoods, large plies |
Reinforcements We Cut
Dry Carbon Fabric
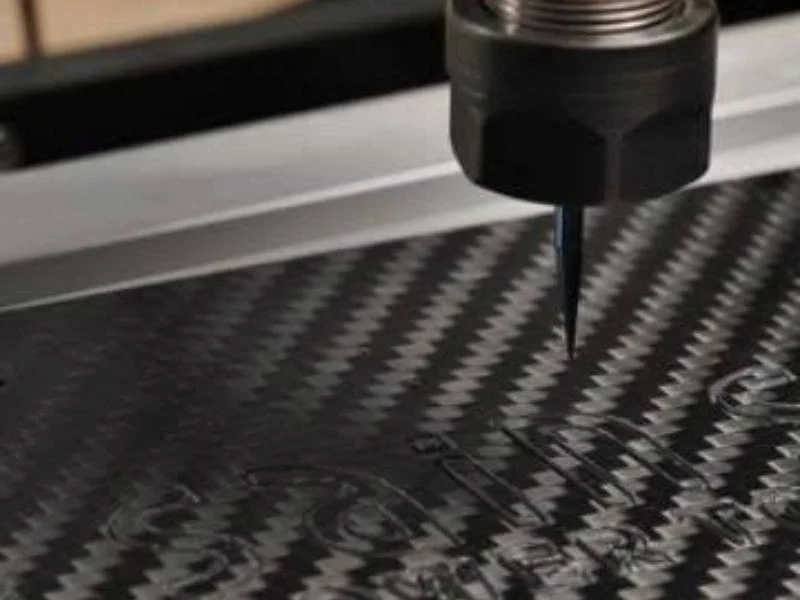
Plain, twill, satin and non-crimp fabric. Cut with a drag blade against the belt so the weave is sheared rather than pulled — no frayed selvedge, no unravelling on the way to the mould.
Carbon Prepreg
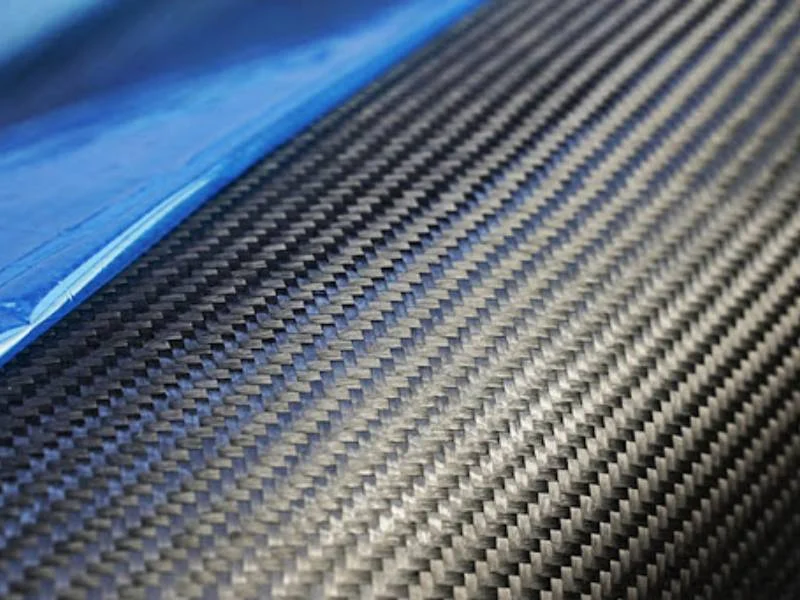
Tacky, cold, and the most expensive material in the shop. Nested tight, cut in one pass, labelled in kit order — and the blade stays clean because it shears instead of dragging resin.
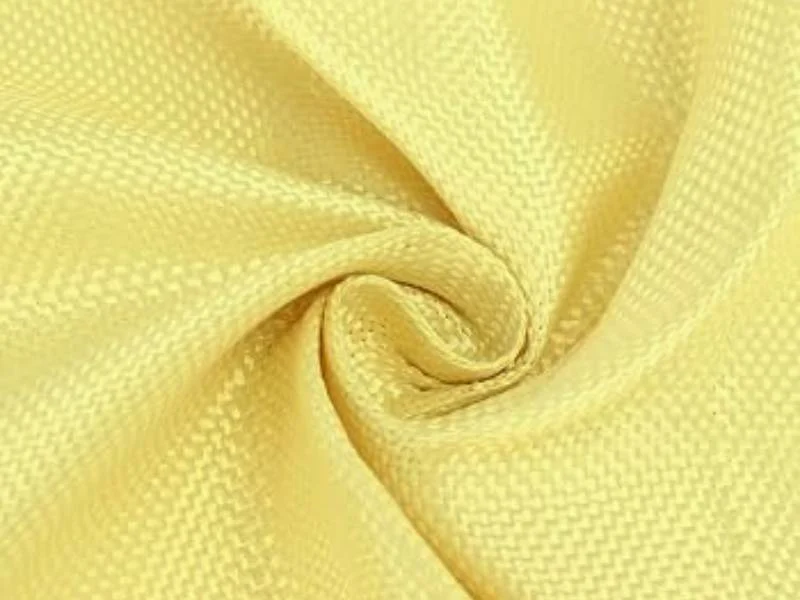
Aramid / Kevlar
The fabric that defeats scissors. A powered oscillating blade cuts aramid without the fuzzing and pull-out that makes hand-cutting it so slow — blade choice matters more here than anywhere.
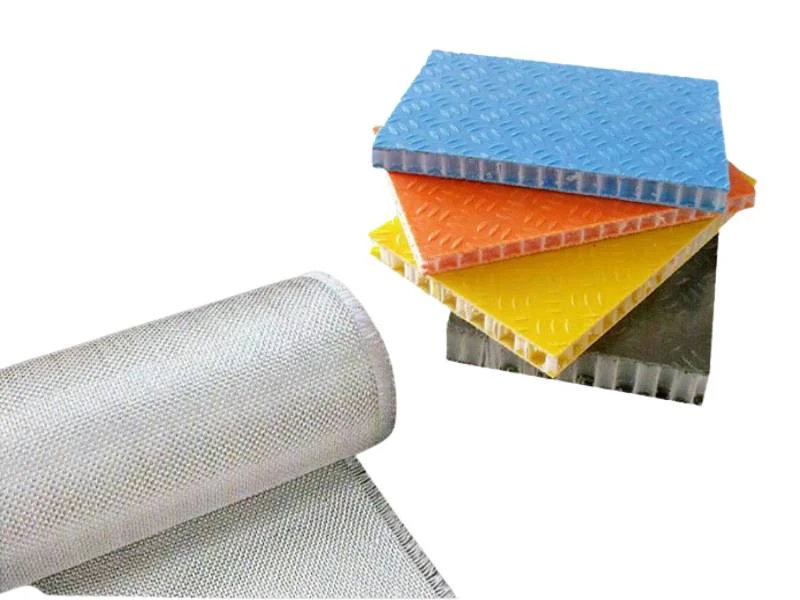
Glass Fabric & Core Materials
E-glass and S-glass reinforcement, plus the honeycomb, foam core and peel ply that go into the same lay-up — one table handles the whole kit rather than three processes.
Who Cuts Composites This Way
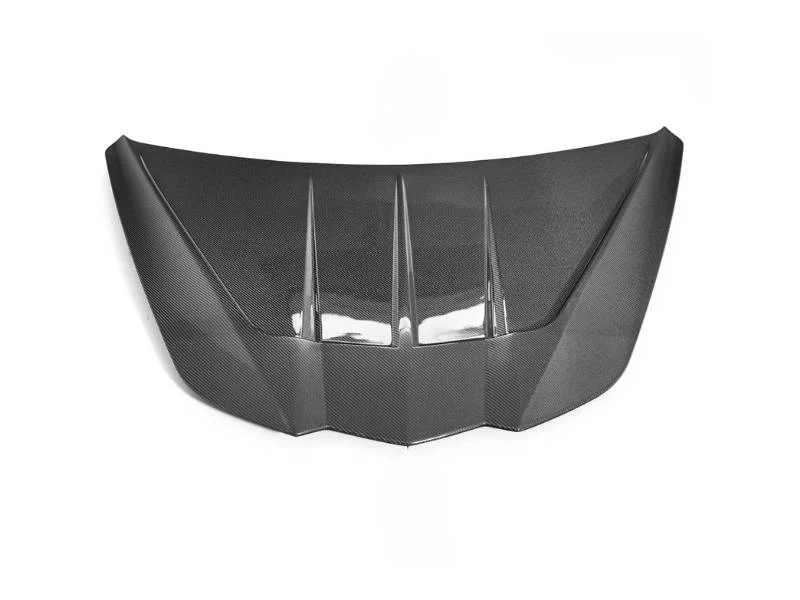
Motorsport & Automotive
Bodywork, aero, monocoque and interior trim plies. Short runs, constant design revisions — a changed ply is a changed file, never a new die.
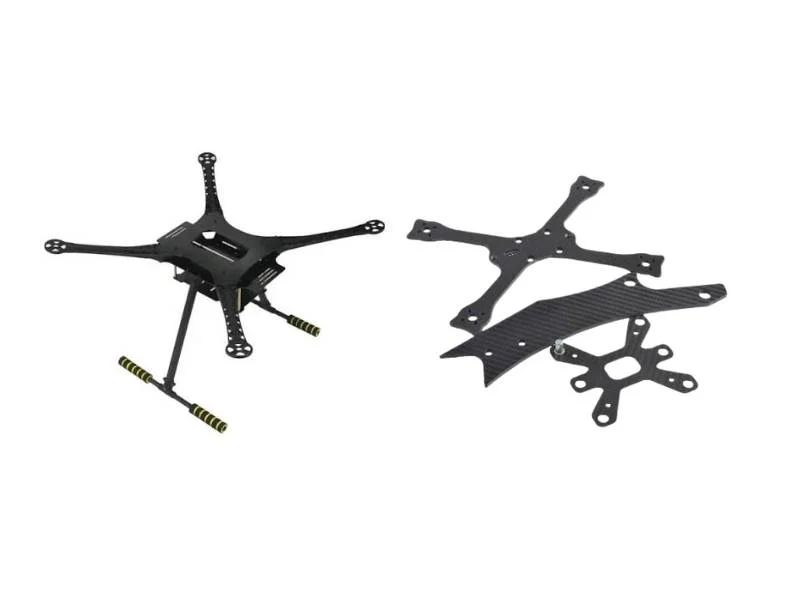
Aerospace & UAV
Ply kits cut to drawing, numbered and traceable. Repeatability and documentation matter as much as the cut itself when the part has to be signed off.
Marine & Wind
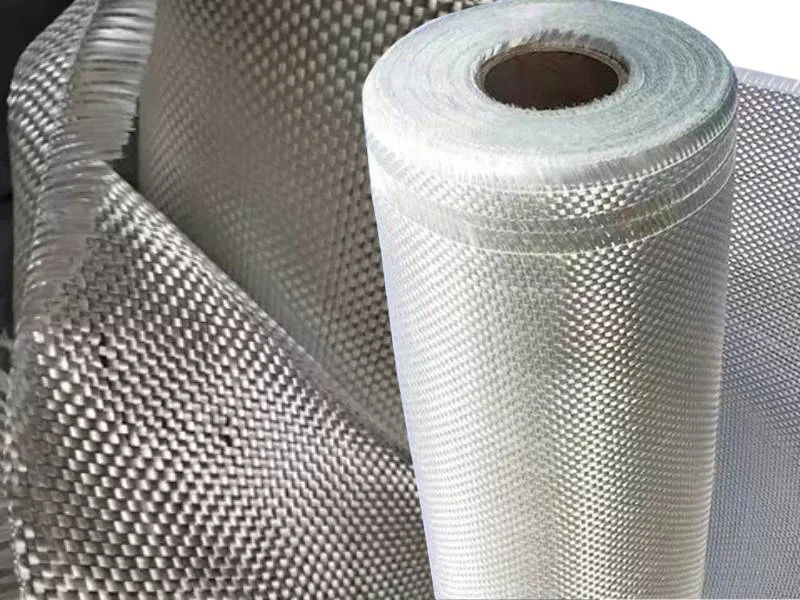
Large glass and carbon plies for hulls, decks and blade shells — the reason table width and conveyor feed matter more than headline cutting speed.
Sporting Goods & Prototyping
Frames, boards, prosthetics and one-off parts. Low volume, high material cost — exactly where nesting yield decides whether the job is profitable.
Recommended MNT Machines
All C-series machines share the same platform, software and tool range — the difference is working size and which tools come fitted as standard.
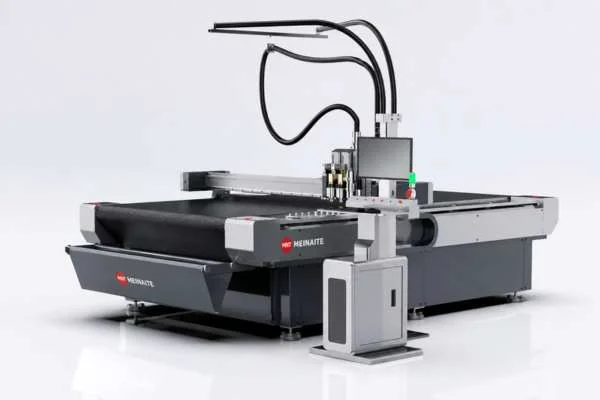
C2516T Digital Cutting Machine
- Cuts: Dry fabric, prepreg, aramid, glass, core materials and peel ply
- Specs: 2500 × 1600 mm · EOT oscillating knife + drag knife + milling spindle · zone vacuum · conveyor feed
- Best for: Production ply kitting where roll goods feed continuously
- Price: From $16,900
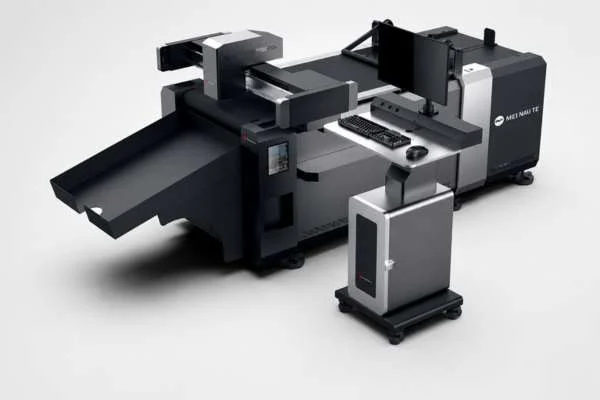
C6090 Digital Cutting Machine
- Cuts: Single-ply carbon and glass fabric, prepreg samples, patterns
- Specs: 600 × 900 / 600 × 1200 / 900 × 1200 mm · EOT + creasing · vacuum table
- Best for: R&D, prototyping and sample rooms rather than the production floor
- Price: From $12,000
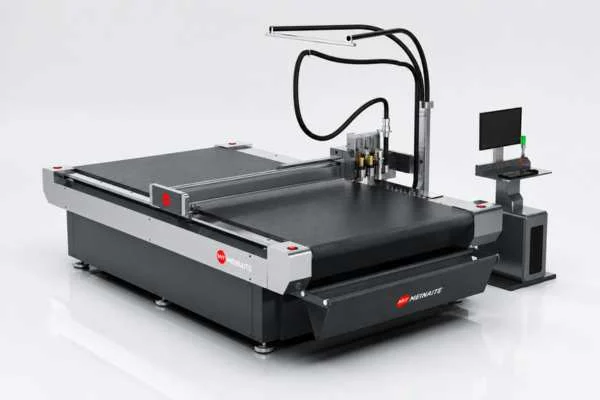
C3232 Digital Cutting Machine
- Cuts: Large glass and carbon plies, wide-roll reinforcement, core sheets
- Specs: 3200 × 3200 mm · POT pneumatic knife + EOT oscillating knife · zone vacuum
- Best for: Marine, wind and any ply too wide for a 1600 mm table
- Price: From $11,555
What a Knife Cutter Will Not Do
The single most common mistake in this category is buying the wrong side of the cure. Here is the split, stated plainly:
| Dry fabric & prepreg (uncured) | Cured CFRP laminate | |
|---|---|---|
| Right process | Oscillating / drag knife | Diamond-coated router or waterjet |
| Why | Material is flexible — a knife shears it cleanly with zero kerf loss | Material is a hard abrasive solid — a knife cannot enter it |
| Typical thickness | 0.2–25 mm single ply or stacked | 1–30 mm laminate |
| Nesting yield | Critical — prepreg is the most expensive material on the floor | Fixed, parts already moulded near-net |
| Edge condition | No fraying if held down and cut in one pass | Risk of delamination and fibre pull-out |
| Dust | Minimal — fibres are sheared, not ground | Heavy conductive dust, extraction mandatory |
| MNT machine | C-series digital knife cutter — this page | Not a knife job — we will say so |
If your work is trimming and drilling cured laminate, a knife table is the wrong purchase — you need diamond-coated routing or abrasive waterjet, and we would rather say that now than after a machine ships. If your work is cutting reinforcement before it goes in the mould, a knife table is not just adequate, it is the only process that costs you nothing in kerf.
Three things that catch first-time buyers
- Blades are a consumable, and carbon eats them. Carbon and aramid are abrasive; budget blade replacement into running cost the way you would budget nitrogen on a laser. Anyone who tells you blade life is a non-issue has not cut aramid.
- Prepreg is a temperature and clock problem. Out-life is consumed from the moment it leaves the freezer, so the table needs to keep up with the kit, not the other way round. Suppliers publish the numbers that decide this — Hexcel and Toray list out-life, tack and areal weight per product, and those three set your realistic cutting throughput.
- Dry carbon dust is electrically conductive. It is far lighter here than on a router, but the extraction and electrical sealing still matter — conductive dust in a control cabinet is a failure mode, not a housekeeping complaint.
Why Composite Shops Choose the C-Series
On composites the machine earns its keep at the vacuum table and the nest, not at the blade. About MNT (MEINAITE) — who builds it and where.
Distributor or OEM partner? Territory, spare-parts commitment and technical training are what decide whether a machine is worth carrying. Talk to us about partnership.
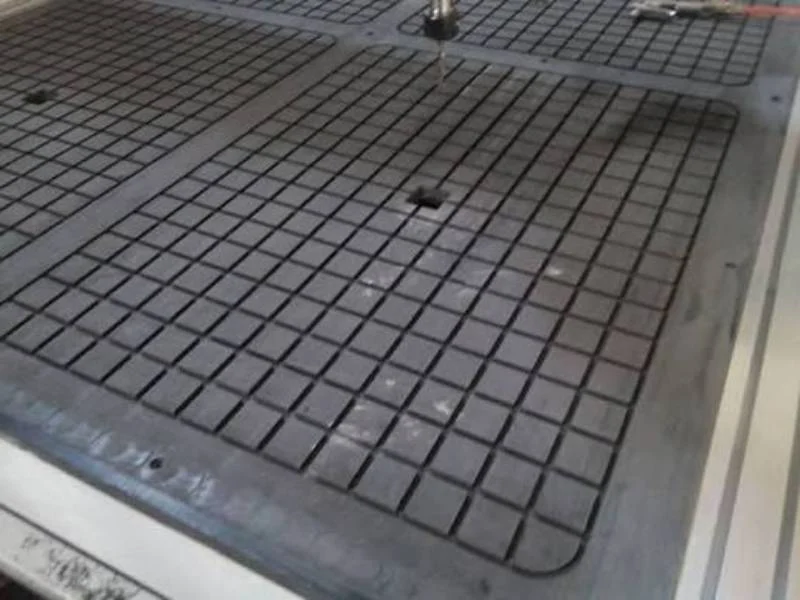
Hold-Down Built for Slippery Material
- Zoned vacuum — suction only where the material is, so it holds instead of leaking
- Conveyor feed for roll goods; the ply never gets lifted and repositioned mid-cut
- Bias-cut and tacky prepreg stay put, which is where hand-cut plies lose their tolerance
- For distributors: composite shops are few but well funded, with long technical evaluations — the sales cycle is slow and the customer, once won, is unusually hard to displace
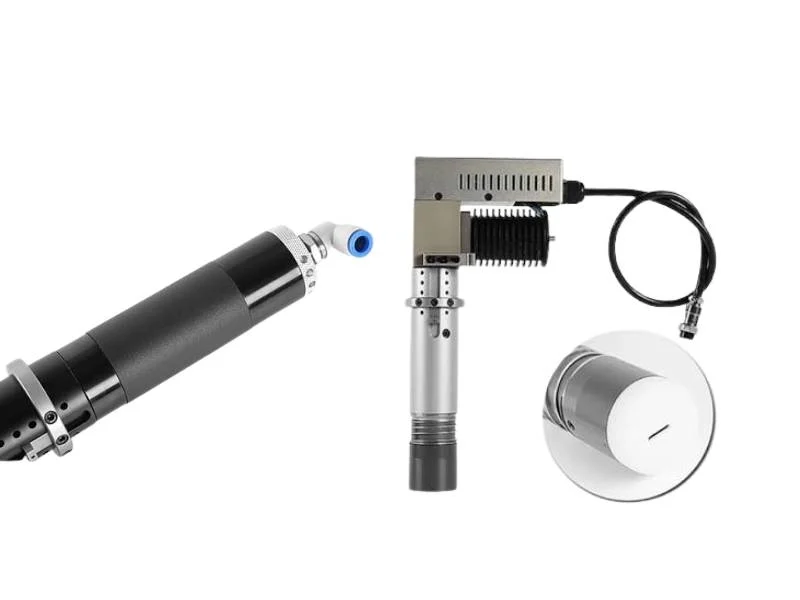
One Head, the Whole Kit
- Oscillating knife, drag knife, creasing and marking tools on the same platform
- Plies come off numbered and in layup order — the part that actually saves hours
- Nesting software rated on yield, because prepreg scrap is the real cost line
- For distributors: spare-parts commitment, territory and technical training are the three things that decide whether a machine is worth carrying — all three are set out on our partnership page
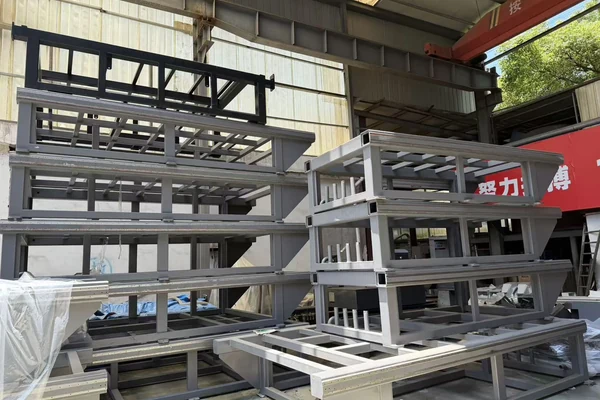
The Factory That Builds Your Ply Cutter
- Frames, gantries and vacuum tables built in-house by Hangzhou Chaohan
- Every machine run-tested and calibrated before shipping
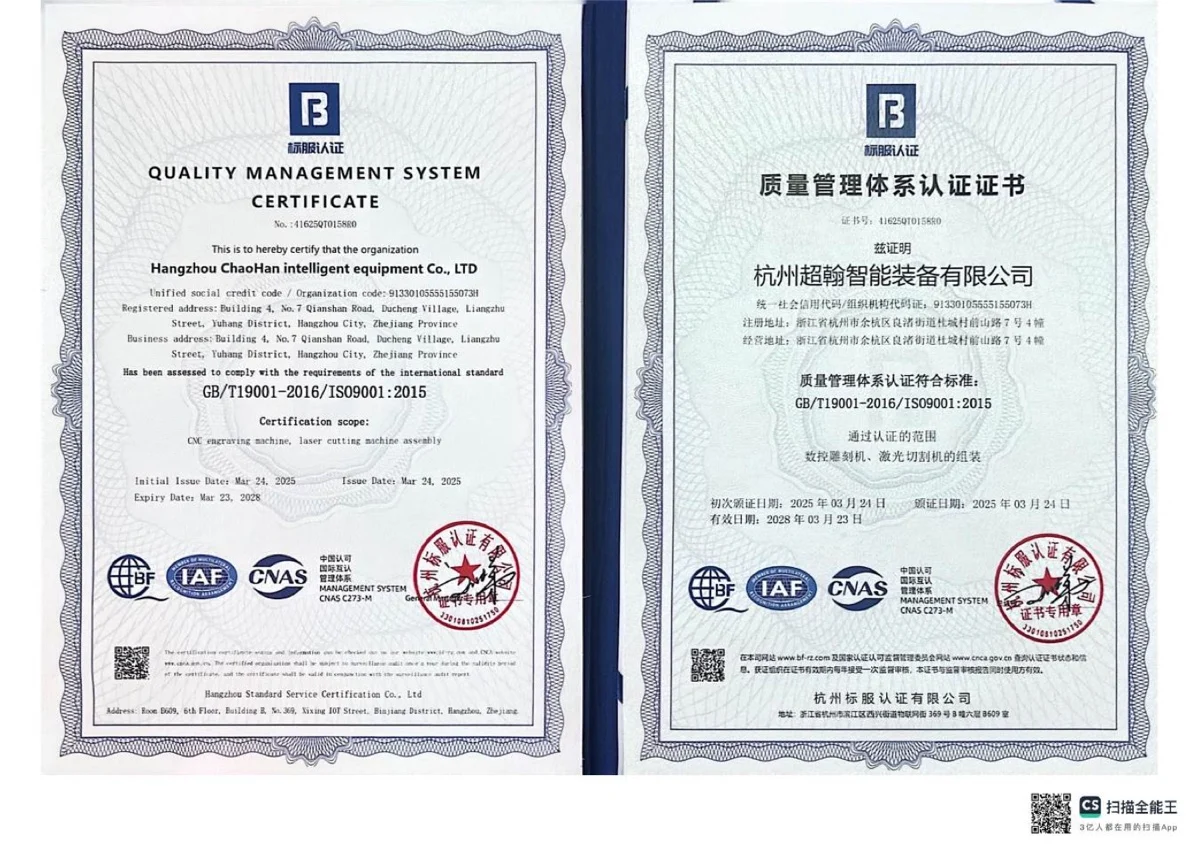
CE + ISO — Send Your Prepreg for a Free Ply Cut
- CE-marked and ISO 9001:2015 certified, built by Hangzhou Chaohan
- Send your fabric or prepreg and a ply drawing — we cut it free and return the plies and edge photos
- 12-month warranty, lifetime software updates, on-site commissioning and training
Sample cuts run on the same C-series build we ship. Send prepreg in its packaging with the out-life noted and we cut and photograph it.
Frequently Asked Questions
Can a knife cutter cut cured carbon fiber laminate?
No. A knife shears flexible material; a cured laminate is a hard abrasive solid the blade cannot enter. Cured parts are trimmed and drilled with diamond-coated routing tools or abrasive waterjet. A digital knife cutter is for the reinforcement before it goes in the mould — dry fabric, prepreg, aramid and glass. Getting this distinction wrong is the most expensive mistake in the category.
Why not laser-cut carbon fiber fabric?
Because heat destroys the resin chemistry. A laser burns and chars the edge, releases fumes from the matrix, and leaves a compromised bond line where the ply meets its neighbour. It also burns away a kerf — on prepreg that costs hundreds of dollars per square metre, that is money the nest never recovers. A blade removes nothing and adds no heat.
How thick a stack can it cut?
An oscillating knife handles roughly 0.2 mm single ply up to about 25 mm of stacked or compressed material, depending on fabric and blade. In practice most composite work is single-ply or shallow stacks, because ply-by-ply accuracy matters more than stacking throughput — a stack that shifts by half a millimetre costs more than it saves.
Does it handle prepreg straight from the freezer?
Yes, and that is the normal way to run it. Prepreg is tacky and cold; the vacuum table holds it and the blade shears rather than drags, so resin does not build up on the tool. The real constraint is out-life — the clock starts when it leaves the freezer, so the table has to keep pace with the kit, and that is a throughput sizing question we work through before quoting.
Can it cut aramid / Kevlar?
Yes — a powered oscillating blade is the standard answer for aramid, which fuzzes and pulls out under scissors or a passive blade. Blade selection and oscillation frequency matter more on aramid than on any other reinforcement, and blade life is shorter. Tell us if aramid is in your material list so we specify the head and the consumable budget correctly.
How much does a carbon fiber cutting machine cost?
A production digital knife cutter with vacuum table and conveyor runs roughly USD 12,000 to 40,000 depending on table size, tool head configuration and whether a camera registration system is fitted. A small sample-room table sits near the bottom; a 3200 mm wide production table with multiple heads near the top. Send your fabric list, ply sizes and monthly volume for a factory-direct quote.
What is the running cost?
Blades, vacuum pump electricity and the cutting underlay. Blades are the line item people underestimate — carbon and aramid are abrasive and consume edges faster than textile or foam work. There is no gas, no abrasive and no consumable optic, which is why total running cost still lands well below a laser or waterjet on the same parts.
Which C-series model fits composite work?
All C-series machines share the same platform, software and tool range — the difference is working size and which tools come fitted as standard. The C6090 suits sample rooms and R&D; the C2516T suits production ply kitting from roll goods; the C3232 exists for plies too wide for a 1600 mm table, such as marine and wind work. See the full digital cutting machine range.
Composite Cutting — Technical Guides
Cured or uncured, knife or diamond tool — the guides behind every recommendation on this page.
Oscillating Knife vs Laser Cutting for Leather: Which Should You Choose?
Why a blade beats a beam on any resin-bearing material: no charred edge, no fumes, no compromised bond line — exactly why carbon prepreg is never laser cut.
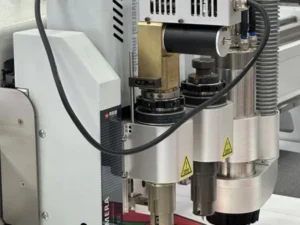
How to Cut Carbon Fiber Without Delamination: Dry Fabric, Prepreg and Fiberglass
Carbon fabric, prepreg and fiberglass each fray differently. Blade choice, vacuum zoning and single-pass cutting for a carbon fiber cutting machine that leaves a clean ply edge.
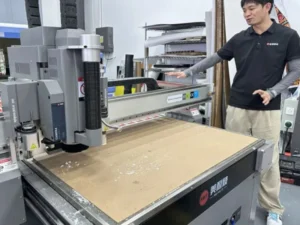
Composite Shops: Ply Cutting and Kitting Workflow
From nest to numbered kit: how ply cutting and labelling shorten layup time in a composite shop — the saving that is never about raw cutting speed.
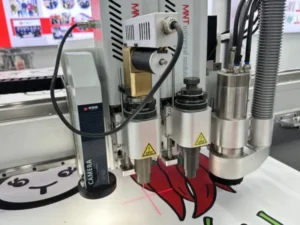
Laser Cutting vs Die Cutting: Which Process Fits Your Material
Three processes, one question: which one matches your material rather than your budget. The chart that separates uncured reinforcement from cured laminate.
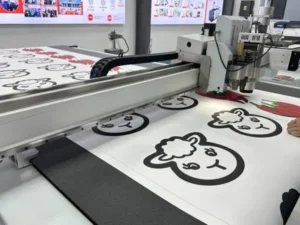
How to Choose a Digital Cutting Table: 12 Questions to Ask Before You Buy
Twelve questions to ask before buying — vacuum zoning, conveyor, tool heads and the specs that quietly decide throughput.
CNC Router vs Waterjet for Thick PTFE Plate
The same process-selection logic that decides how a cured composite part gets trimmed once it leaves the mould.
Send Us Your Fabric for a Free Ply Sample Cut
Send a ply drawing and your reinforcement — dry fabric, prepreg or aramid. We cut it on a C-series, return the plies and edge photos, and tell you honestly if a knife is the wrong process for your part.